Why Choose a Shuttle Rotomolding Machine?
Choosing the right equipment can shape production quality, labor efficiency, and long-term operating costs. A Shuttle Rotomolding Machine offers a practical solution for manufacturers producing large, hollow plastic parts. Its two independent arms allow loading and unloading on one side while another mold remains inside the heating or cooling chamber. This reduces idle time and supports a steadier workflow.
In real production environments, small details matter. Operators may handle steel molds beside the machine, inspect wall thickness, and remove parts while surfaces are still warm. A well-designed Shuttle Rotomolding Machine can improve access, visibility, and process control during these tasks. Temperature monitoring, reliable arm movement, and consistent mold rotation help reduce common defects such as uneven walls, trapped air, and incomplete corners. These benefits are especially valuable for tanks, containers, playground components, and industrial housings.
Still, no machine solves every production problem. Poor mold design, unsuitable resin, or weak cooling practices can limit results. That deserves attention. Equipment selection should consider part size, mold weight, cycle time, factory layout, energy use, and operator training. Experienced manufacturers also review service support and replacement parts before purchase. A lower initial price may not remain economical after repeated downtime. This article examines why the Shuttle Rotomolding Machine remains a trusted choice for flexible production, while also identifying its practical limitations. The goal is clear: informed decisions, measurable performance, and safer daily operation.
What Is a Shuttle Rotomolding Machine?
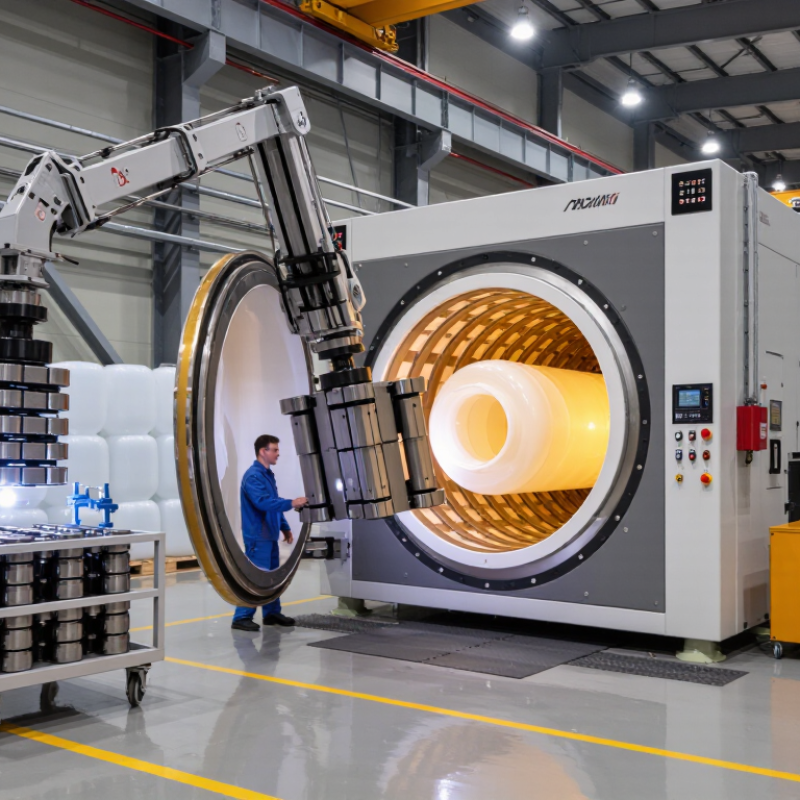
A shuttle rotomolding machine is a rotational molding system with two or more arms. Each arm carries a mold between separate stations. These stations usually include heating, cooling, loading, and unloading areas. The mold receives measured polymer powder, then rotates inside an oven. Heat melts the powder against the mold wall and forms a hollow product.
Unlike a fixed-arm machine, a shuttle design can move one mold into the oven while another cools outside. This arrangement supports shorter handling times and better production flexibility. Operators can inspect a cooled tank, add powder to another mold, and prepare the next cycle nearby. The process suits water tanks, pallets, ducts, and large industrial containers. Grand View Research estimates the global rotational molding market will expand at about 4.8% annually through 2030. Mordor Intelligence also forecasts continued growth, linked to demand for lightweight, corrosion-resistant plastic products.
In practice, shuttle equipment needs careful temperature control and mold balancing. Uneven powder distribution can create thin corners or weak seams. That detail is easy to underestimate. A larger machine is not automatically better. It may consume more energy and require longer cooling time. Real production trials should measure cycle time, wall thickness, scrap rate, and operator movement. These checks often reveal that a simpler setup performs better for a specific product. Industry recommendations from the Association of Rotational Molders also emphasize process control, mold design, and repeatable heating conditions.
Why Choose a Shuttle Rotomolding Machine?
A shuttle rotomolding machine uses a mobile mold carriage that moves between the heating chamber and service areas. This layout supports separate loading, unloading, and cooling activities while another mold is inside the oven.
Representative two-arm shuttle layout: The chart shows the typical number of key stations or moving elements in a standard shuttle-machine arrangement. Two service positions and two mold arms help operators handle molds outside the oven, while one central oven provides controlled heating. Actual configurations vary by machine size, mold weight, and production requirements.
How Does a Shuttle Rotomolding Machine Work?
Why Choose a Shuttle Rotomolding Machine?
How Does a Shuttle Rotomolding Machine Work?
A shuttle rotomolding machine uses two movable carriages. Each carriage carries one or more molds. While one carriage enters the heating chamber, the other stays outside for loading, cooling, and demolding. This arrangement keeps production moving and reduces waiting time between cycles.
The operator places a measured amount of polymer powder inside a hollow mold. The mold closes and moves into the oven. It rotates around two axes during heating, spreading the softened material across the inner surfaces. Heat sensors and cycle controls help maintain stable processing conditions. The mold then leaves the oven and enters a cooling area. Air or water mist removes heat gradually, while rotation continues to prevent uneven wall thickness. Once the part becomes firm, the operator opens the mold and removes it.
This process suits tanks, containers, playground parts, and other large hollow products. It creates seamless walls with relatively low forming stress. Shuttle movement also allows different molds to follow separate cycle times. That flexibility can support small batches and varied designs.
Real production still needs judgment. Powder quality, mold temperature, and cooling speed can change the final result. A perfect setting rarely exists. Operators may need to adjust the cycle after inspecting corners, vents, and wall thickness. Poor loading can create thin areas, even when the machine runs correctly. Careful records and regular maintenance make the process more reliable.
What Are Its Main Design and Operating Features?
A shuttle rotomolding machine uses a movable carriage to serve one or more stations. Its main advantage is controlled movement between heating and cooling areas. The carriage typically carries two molds, allowing loading while another mold cools. This layout can reduce idle oven time. It also supports flexible production for tanks, pallets, containers, and large hollow parts.
The design depends on biaxial rotation, adjustable arm speed, and accurate mold indexing. A PLC records oven temperature, rotation cycles, and cooling duration. These controls help operators repeat wall thickness and reduce uneven surfaces. According to Grand View Research’s 2024 rotational molding market report, the sector is expected to grow at roughly 5% annually. That growth increases pressure for stable, data-based processing. Still, automation does not remove every problem. Powder quality, mold venting, and loading accuracy remain critical.
Operating discipline matters just as much. Operators charge a measured polymer weight, close the mold, and check the locking system before heating. The mold then rotates through a programmed thermal cycle. After heating, controlled air or water cooling limits distortion. The U.S. Department of Energy notes that poorly maintained compressed-air systems can waste 20–30% of supplied air, so pneumatic leaks deserve regular inspection. In practice, some plants still adjust cycles by experience alone. That approach can work, but it is difficult to audit. A shuttle machine performs best when temperature records, mold condition, and cooling results are reviewed together.
Why Choose Shuttle Rotomolding for Plastic Production?
Shuttle rotomolding gives plastic producers a practical way to manage several mold stages in one working area. Two or more shuttle arms move molds between heating, cooling, and loading stations. This layout can reduce idle time while operators prepare the next mold. In daily production, that matters. A large insulated mold may need careful cooling, while a smaller part is ready for loading. Separate movement paths make timing easier to control. The result is flexible production for tanks, containers, housings, and custom parts.
The process also supports consistent wall thickness when operators control temperature, rotation speed, resin quantity, and cooling conditions. Good records help connect surface defects to real process changes, rather than guesswork. Operators can inspect molds, verify vent placement, and remove flash before the next cycle. These details reflect practical experience, not only machine specifications. Shuttle systems may also simplify mold changes when product sizes vary during the week. Less manual repositioning can improve handling safety and reduce avoidable damage.
Still, shuttle rotomolding is not automatically the best answer. Its benefits depend on accurate cycle planning, trained operators, and disciplined maintenance. Poorly balanced molds can create uneven heating or unnecessary movement. Production plans may look efficient on paper, yet lose time through awkward loading access. That weakness deserves honest review before investment. Energy use, floor space, tooling weight, and annual volume should be measured with actual shop data. A careful trial run can reveal more than a polished quotation.
 (780) 669-9420

